How to Choose a Cutting Fluid: A Guide by Material and Operation
The right cutting fluid drives tool life, surface quality and cost per part. A step-by-step selection by material, operation and machine.
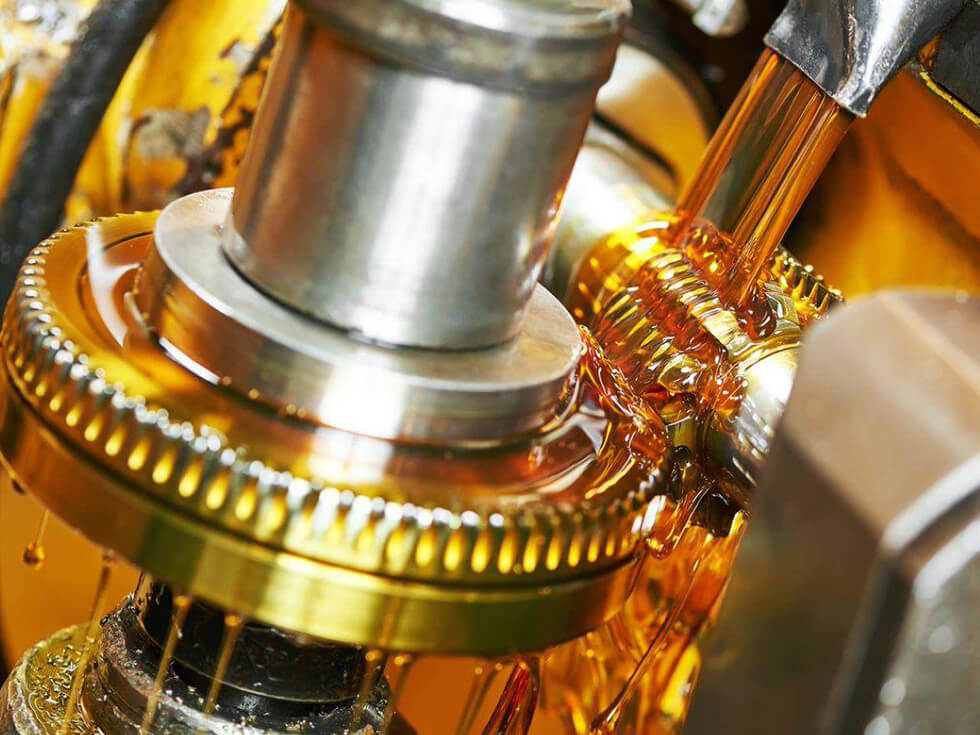
In most workshops cutting fluid is chosen by looking at the price list. But the wrong fluid comes back within weeks as broken tools, poor surface finish, odour and rust complaints. The right choice starts with three questions: which material, which operation, which machine.
1. Start with the material
The workpiece material sets the fluid chemistry. Alloy and stainless steel need extreme-pressure (EP) additives and strong lubrication; aluminium and copper need low-pH, non-staining formulas that do not discolour the metal. For cast iron, chip and sludge management comes first.
2. Operation severity
Light turning and milling are handled by water-based (emulsion) fluids. Heavy operations such as tapping, broaching, deep-hole drilling and honing benefit clearly from neat cutting oil or high-concentration emulsion. In grinding, filterability and foam control are critical.
3. Water-based or neat oil?
- —Water-based (emulsion): Good cooling, high speed, lower cost. Requires maintenance (concentration, pH).
- —Neat cutting oil: Superior lubrication and finish, long life. Weaker cooling, higher cost.
4. Machine and water quality
Central system or individual sump? Water hardness directly affects emulsion stability; hard water causes foam and soap formation. Seal and paint compatibility specified by the machine builder should not be ignored.
Decision summary
First define material + operation, then decide water-based vs neat, and finally set the concentration and maintenance plan. If in doubt, a trial on one machine with a sample is the safest route.
At Ahmet Ceviz we measure concentration and pH on site and recommend the product that fits your operation. Use the product finder or request a sample directly.